Scaling a Candle Range From 500 to 5,000 Units
You have been pouring a 500-unit candle run by hand in a double boiler, and it works. The moment you accept an order for 5,000 units, every shortcut that was invisible at small scale becomes a defect: wax sits too long in the pot, fragrance
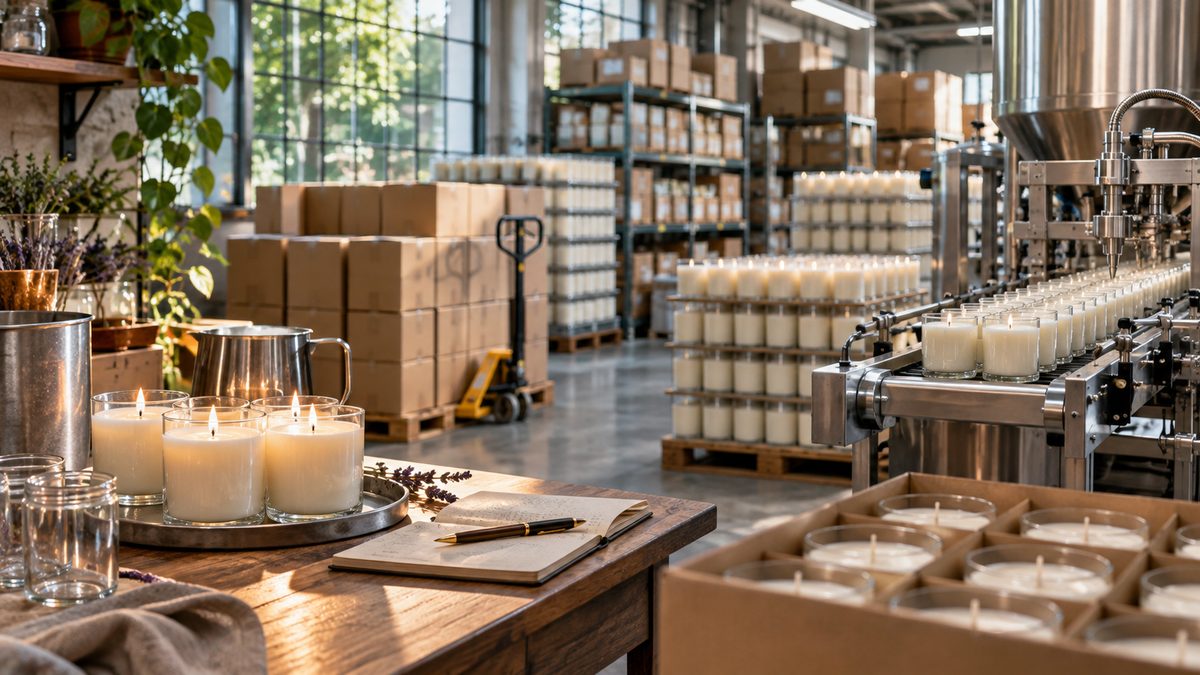
You have been pouring a 500-unit candle run by hand in a double boiler, and it works. The moment you accept an order for 5,000 units, every shortcut that was invisible at small scale becomes a defect: wax sits too long in the pot, fragrance burns off, wicks wander off-centre and a whole pallet arrives with uneven burn pools.
This article explains what actually changes when a candle line grows tenfold, from wax conditioning and pour temperature to wick centring, cure time and quality sampling. It gives you a step-by-step route for moving from a kitchen-scale process to a repeatable production line without losing the scent throw your customers bought the first time.
Table of Contents
- Where the 500-unit process breaks
- Wax melting and conditioning at volume
- Wick selection and centring at scale
- Fragrance load and batch consistency
- Cure time is inventory, not waiting
- What to test at 5,000 units
- Practical guide: moving a candle line from 500 to 5,000 units
- Frequently asked questions
- Conclusion
Where the 500-unit process breaks
A double boiler melts maybe ten kilograms of wax at a time. At 150 grams per candle, that is about sixty units per pot. To hit 5,000 units you need roughly eighty pots, and each pot carries the same risk: the wax temperature drifts, the fragrance is added at a different point, and the last candles poured from a cooling pot are not the same as the first.
The bottleneck is the pot, not the people
Scaling is not a matter of pouring faster; it is a matter of removing the temperature and time variance that a small pot hides. Identify the step that forces you to wait or to compromise on temperature, and that step is where the new line has to change first.
Wax melting and conditioning at volume
At scale you move from a pot to a jacketed melting tank with a stirrer and a temperature controller. The jacket heats evenly, the stirrer keeps fragrance and dye dispersed, and the controller holds the wax within a few degrees of the target instead of swinging as a hotplate cycles on and off.
Pour temperature is a window, not a number
Each wax has a recommended pour range. Pour too hot and the candle develops sink holes and frosting as it cools; pour too cool and the fragrance does not bind and the surface turns lumpy. Write the pour range into the work instruction and check it with a probe at the nozzle, not at the tank.
Flash point versus pour temperature
Fragrance oils have a flash point, and the melt must stay far enough below it that the vapour above the tank cannot ignite. This is a safety ceiling, not a quality target. Keeping the wax well under the flash point also slows fragrance evaporation, so a lower holding temperature protects both safety and scent.
Wick selection and centring at scale
At 500 units you can eyeball a wick into the centre of the jar. At 5,000 units a wick that sits two millimetres off-centre changes the melt pool and produces tunnelling or a hot spot on the glass, and those complaints arrive weeks after you have shipped.
Centring fixtures beat steady hands
A simple jig that holds the wick tab in place while the wax sets removes the largest single source of variance. The wick must also stay vertical through cooling, so the fixture should grip the wick at the top and bottom rather than relying on the tab alone.
Fragrance load and batch consistency
Fragrance load is the percentage of fragrance oil added to the wax, and it is the number that decides both throw and cost. When you scale up, the same nominal load can drift because a large batch is harder to mix thoroughly, and the fragrance can pool at the bottom of an unstirred tank.
Add fragrance at a fixed temperature
Stir the fragrance in below the flash point but above the wax's solidification point, and hold the stir for a set time on every batch. Document the load as a weight, not a volume, because fragrance oils vary in density and a measuring jug is not a scale.
Cure time is inventory, not waiting
A soy or blended wax candle does not reach its final throw the day it is poured. The fragrance needs time to bind into the wax crystal structure, and that means a 5,000-unit order occupies shelf space for days before it can ship.
Plan the cure into the lead time
Decide your cure window by test, not by guess, and build it into the schedule so you are not selling candles whose throw will strengthen after the customer has already judged them. Cure time is a production stage with a space cost, and scaling without planning for it is how pallets pile up.
What to test at 5,000 units
The tests that matter at volume are the ones that catch a bad batch before it leaves the floor: pour weight, wick position, surface condition, and a burn test on a sample from each melt. A burn test takes hours, so you sample rather than test everything.
AQL sampling instead of 100% inspection
Use an acceptance sampling plan so you inspect a defined number of units per lot and accept or reject the lot on the result. Test cold throw on the line and burn a smaller sample for hot throw, melt pool and sooting, because those three are what the end customer will notice first.
| Test | What it catches | When to run |
|---|---|---|
| Pour weight | Under- or over-fill | On the line, sampled per lot |
| Wick position | Off-centre burn | On the line, sampled per lot |
| Burn test | Melt pool, sooting, hot throw | On a subset from each melt |
| Parameter | 500-unit method | 5,000-unit requirement |
|---|---|---|
| Wax melting | Double boiler, small pot | Jacketed tank with stirrer and controller |
| Fragrance addition | Eyeballed by volume | Weighed load at fixed temperature |
| Wick centring | By hand | Centring jig, top and bottom grip |
| Quality check | Every candle | AQL sample plus burn test |
Practical guide: moving a candle line from 500 to 5,000 units
Step 1 — Map the current bottleneck
Time each step on the existing line and mark the one that forces waiting or temperature compromise. That step is your first investment target, not the step that merely looks slow.
Step 2 — Lock the wax, wick and load spec
Write down the wax, the wick series, the jar and the fragrance load as a fixed specification before you scale, so the bigger line reproduces the candle you already sell.
Step 3 — Move to a jacketed tank
Replace the pot with a jacketed, stirred, temperature-controlled melter and set the hold and pour ranges in the work instruction.
Step 4 — Build centring and clipping fixtures
Make a jig that holds each wick centred and vertical through cooling. This single fixture removes most of the burn-pool defects that appear at volume.
Step 5 — Set cure and burn-test gates
Define the cure window and a burn-test gate on samples from each melt, so no lot ships before it has been checked for melt pool, hot throw and sooting.
Step 6 — Adopt an AQL sampling plan
Replace 100% inspection with a defined sample size per lot and a clear accept/reject rule for weight, wick position and surface defects.
Step 7 — Run a pilot batch first
Pour a small pilot run on the new line, burn-test it against your 500-unit reference, and only then release the full 5,000-unit order.
Frequently asked questions
What is candle production scaling?
Candle production scaling is the process of taking a candle from small-batch, manual production to a larger repeatable line. It is not just pouring more; it means removing temperature, mixing and placement variance so every candle matches the approved sample.
What is fragrance load in candles?
Fragrance load is the percentage of fragrance oil added to the wax by weight. It determines scent throw and cost, and it must be controlled precisely because too little gives weak throw and too much can cause seepage or poor burning.
What is a candle burn test?
A burn test lights a finished candle and measures melt pool diameter, flame height, sooting and hot throw over time. It is the standard way to verify that a wick and wax combination burns safely and evenly.
Why does scent throw drop when I scale up the batch?
Throw usually drops because fragrance is not fully mixed into a larger volume or is added at the wrong temperature and partially evaporates. A stirred, temperature-controlled tank and a weighed fragrance load restore the throw of the small batch.
How long should candles cure before shipping?
The cure window depends on the wax; soy and soy blends typically need several days to reach full throw. Determine the window by burn test rather than guesswork, and build it into the lead time as inventory.
What sampling plan should I use for 5,000 candles?
Use an acceptance sampling plan with a defined sample size per lot, testing pour weight, wick position and surface on the sample and running a burn test on a smaller subset for melt pool, hot throw and sooting.
Do I need a jacketed melter at 5,000 units?
For most waxes, yes. A jacketed tank with a stirrer and controller is the cheapest way to remove the temperature swings that cause frosting, sink holes and inconsistent throw across a large run.
When should I automate wick placement?
Automate wick placement when manual centring becomes the bottleneck or the defect source. Before that, a centring jig delivers most of the quality benefit at a fraction of the cost of a machine.
Conclusion
Scaling a candle line is a process of removing variance, not a matter of buying a bigger pot. The three levers that carry you from 500 to 5,000 units are a temperature-controlled melt, a centred and vertical wick, and a weighed fragrance load mixed at the right temperature.
Plan the cure window as inventory and replace 100% inspection with a sampling plan that catches burn defects before shipping. If you want to hand the whole transition to a manufacturer that already runs at this volume, contact us to discuss your range, or review our candle packaging options and the combustion science behind wick and wax choice.
Discuss your fragrance programme with our team:
WhatsApp: +86 17324762943
Email: adon@customperfumeoem.com
Website: customperfumeoem.com