Custom Candle Lids: Tooling, Lead Time and Cost Against Stock
A brand picks a stock lid from a catalogue, builds a whole range around it, and then watches a competitor launch the same jar with an engraved wooden lid that makes the product look twice the price. Or the reverse: a buyer commissions a cus
A brand picks a stock lid from a catalogue, builds a whole range around it, and then watches a competitor launch the same jar with an engraved wooden lid that makes the product look twice the price. Or the reverse: a buyer commissions a custom lid, pays the tooling, and realises at 3,000 units that the per-unit cost will never break even against the stock part.
This article lays out how custom candle lids are made, what drives tooling cost, how lead times and minimum orders actually behave, and where the break-even sits against stock lids. It covers materials, tooling methods, quality checks, and the questions to ask before you pay for a mould.
Table of Contents
- Stock lids versus custom lids
- Lid materials and their tooling
- Tooling types and cost drivers
- Lead time and minimum order quantity
- Quality checks on lids
- When a custom lid pays off
- Practical guide: specifying and budgeting a custom candle lid
- Frequently asked questions
- Conclusion
Stock lids versus custom lids
A stock lid is an existing moulded part the factory already owns: the standard bamboo disc, the brushed aluminium screw-top, the glass dome. You buy it at catalogue price with no tooling charge, and it ships in days. The trade-off is that it is not yours — the same lid sits on shelves in three other brands' ranges, and you cannot change its finish, dimension, or logo without moving to a custom part.
A custom lid is made to your drawing, typically through a new mould or a machining program. You pay for tooling once, then own an exclusive part, but you also own the inventory risk: minimum order quantities apply per finish, and a slow-selling SKU leaves you holding lids that fit only your jar. It is a working-capital question with a tooling amortisation attached.
Lid materials and their tooling
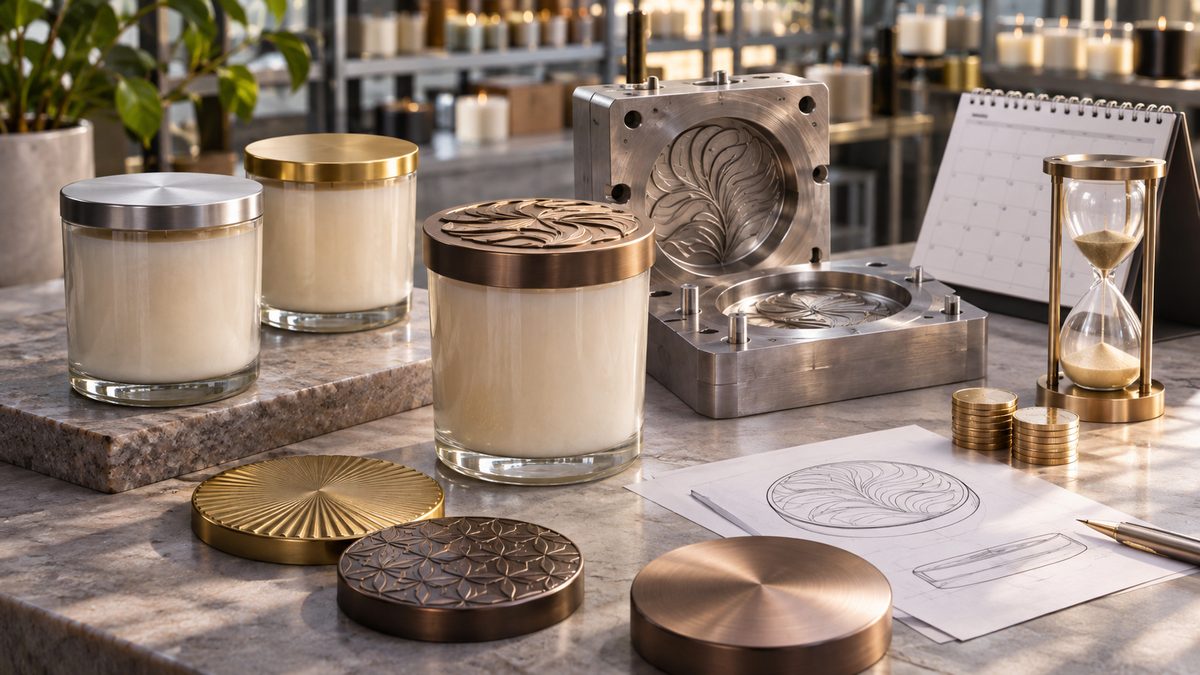
Each material carries a different tooling cost and production method, which is why "custom lid" is not one thing. Wood lids — bamboo, pine, or beech — are usually CNC-machined and laser-engraved, so tooling is cheap but per-unit labour is high. Metal lids are stamped or die-cast; a stamped tin die is modest, while a die-cast zinc-alloy lid with fine detail is the most expensive in the category.
Finish and decoration
Decoration often costs more than the lid itself. Embossing needs the logo cut into the tool, debossing the reverse, and printing, engraving, or hot-stamping are separate post-processes. A plain custom lid can undercut a decorated stock lid, while a fully decorated custom lid can triple the base part price. Decide the decoration spec before comparing quotes.
Fit is a hidden specification
The lid must mate with the vessel's thread or rim within a tight tolerance, and a lid made to "roughly" the jar dimension is a common failure. Specify the vessel, its measured mouth diameter, and the required interference or thread pitch, and ask for a fit sample on your actual jar before tooling is cut. A lid that wobbles on the real jar is scrap.
Tooling types and cost drivers
Tooling cost is set by material, cavity count, and the level of surface detail, not by the size of the lid. A simple stamped tin lid needs a single forming die, while a die-cast metal lid needs a hardened multi-cavity mould with ejectors and cooling. Wood needs no mould at all but requires a CNC program and often a jig for repeatability.
| Lid type | Tooling approach | Relative tooling cost | Per-unit cost driver |
|---|---|---|---|
| Wood (bamboo, beech) | CNC machining, laser engraving | Low | Machine time, finishing labour |
| Stamped tin / aluminium | Forming die | Low to moderate | Material, coating |
| Injection-moulded resin | Plastic injection mould | Moderate | Cavity count, cycle time |
| Die-cast zinc alloy | Die-cast mould | High | Plating, polishing, detail |
| Glass lid | Glass mould | Moderate to high | Annealing, clarity spec |
The single largest controllable cost lever is cavity count. A one-cavity mould is cheap to cut but slow to run; a multi-cavity mould costs more up front and pays back quickly at volume. Ask the factory for the cycle time and the piece rate at each cavity count, not just the tooling quote, because a cheap mould with a slow cycle can cost you more by the third order.
Lead time and minimum order quantity
Lead time splits into tooling time and production time. Tooling for a stamped metal lid can be cut in weeks; a die-cast mould with polishing can take longer, and any revision after first samples restarts the clock. Production lead time then depends on decoration, plating, and finishing, which are the steps buyers most often forget to count.
Minimum order quantity is usually stated per finish and per colour, not per design. A lid offered in three wood stains may carry three separate MOQs, which can quietly triple the working capital you need. Confirm whether the MOQ applies to the raw part or to the decorated lid, and whether you can run unprinted lids now and decorate them later to spread the commitment.
Quality checks on lids
Lid defects are visually loud — a scratched finish, a wobbling fit, or an off-centre logo reads as a quality problem on the whole candle. Because the lid is the first thing a customer touches, the inspection standard should be stricter than the one you apply to the wax fill. Define the acceptable defect classes before production and put them in the purchase spec.
| Check | What it catches | Method |
|---|---|---|
| Fit on vessel | Oversize, undersize, thread mismatch | Gauge or trial assembly on real jar |
| Finish uniformity | Plating streaks, stain blotches | Visual under standard lighting |
| Logo position | Off-centre or rotated engraving | Template or jig overlay |
| Coating adhesion | Peeling, chipping at edges | Cross-hatch tape test |
| Weight and hardness | Thin walls, soft metal | Scale and hardness gauge |
Inspection checks and approval
Approving against a golden sample
Keep a signed golden sample of the lid — the exact part, finish, and decoration you approved — and reference it in the spec. QC against the golden sample, not against memory or a photo, because a render and a plated part rarely match. When the factory proposes a process change, such as a different plating vendor, re-approve against the golden sample before you accept the batch.
When a custom lid pays off
Custom tooling pays when the amortised cost per lid is below the premium you can charge, and the maths is straightforward. Take the tooling cost, divide it by the number of lids you will realistically sell in the product's life, and add the per-unit cost. If the result is materially below the price uplift the exclusive lid supports, the project clears; if it only clears at a volume you have never hit, the stock lid is the honest answer.
Custom lids also earn their cost through exclusivity alone in some channels. In gift sets and premium retail, a lid that cannot be bought off a competitor's shelf is part of the brand defence. For planning how lid choices fit a wider range, see our candle pack planning guide and the packaging options we stock, and confirm how changing a lid interacts with EU packaging rules in our compliance note.
Practical guide: specifying and budgeting a custom candle lid
Step 1 — Fix the vessel first
Finalise the jar and measure the actual mouth diameter and thread. A lid is specified against a vessel, and every jar change invalidates the lid tooling.
Step 2 — Choose material and decoration together
Pick the material and the finish in the same decision, because decoration is the largest variable in both cost and lead time.
Step 3 — Get the cycle-time economics, not just the tooling quote
Ask for cavity count, cycle time, and piece rate at your volume. Amortise tooling across a realistic lifetime, not an aspirational one.
Step 4 — Order a fit sample before tooling
Require a sample lid on your actual jar and approve it in writing. This is the cheapest moment to catch a fit error.
Step 5 — Write the defect classes into the spec
Define acceptable and rejectable defects, fix the inspection standard, and attach a golden sample reference.
Step 6 — Confirm MOQ per finish and the decoration schedule
Lock the minimum order per stain, colour, and decoration, and agree whether undecorated lids can be held in stock.
Frequently asked questions
What is private label candle manufacturing?
Private label candle manufacturing is when a factory produces candles under your brand name using your chosen wax, fragrance, vessel, lid, and packaging. The manufacturer handles production and quality control, while you own the brand and the route to market.
What is a candle lid?
A candle lid is the cover that protects the wax, preserves cold throw between burns, and finishes the product's look. Lids come in wood, metal, glass, resin, and ceramic, in both stock and custom versions.
What is tooling in candle manufacturing?
Tooling is the mould, die, or machining program used to make a custom component such as a lid or vessel. It is a one-time cost you pay up front and then amortise across the units produced from it.
How much does a custom candle lid mould cost?
It depends on material and complexity rather than size. A CNC wood lid needs little tooling, a stamped tin die is modest, and a polished die-cast metal mould is the most expensive. Ask for the cycle-time economics, not the tooling number alone.
What is the minimum order quantity for a custom lid?
MOQ is usually stated per finish or colour, so a lid in three stains can carry three separate minimums. Confirm whether the MOQ applies to the raw or the decorated part before you commit.
Can I start with a stock lid and switch to custom later?
Yes, but only if the vessel mouth is unchanged. If the custom lid needs a different jar, the switch also changes your vessel, label, and fill spec, so plan the transition as a single change rather than a lid swap.
What is the most common custom lid defect?
Fit is the most common, followed by finish inconsistency. A lid that wobbles on the real jar or shows plating streaks is a reject; both are caught with a fit sample and a golden-sample inspection standard.
How do I know if custom tooling will break even?
Divide the tooling cost by the realistic lifetime volume and add the per-unit cost, then compare against the price premium an exclusive lid supports. If the maths only works at a volume you have never sold, the stock lid is the safer call.
Conclusion
A custom lid is a working-capital decision with a finish problem attached, not a pure design decision. The tooling charge is the visible cost, but the real expenses are the per-finish minimums, the decoration steps, and the inventory of a part that fits only your jar.
The disciplined sequence is vessel first, then material and decoration as one choice, then a fit sample on the real jar before any mould is cut. The break-even maths then tells you plainly whether the exclusivity is worth it.
Discuss your fragrance programme with our team:
WhatsApp: +86 17324762943
Email: adon@customperfumeoem.com
Website: customperfumeoem.com