Amortising Mould Cost Across Car Fragrance SKUs
A brand orders three car fragrance SKUs, each with its own injection mould, and ends up carrying three tooling charges that will never amortise at the volumes the line actually sells. Or the reverse: a brand forces five different shapes int
A brand orders three car fragrance SKUs, each with its own injection mould, and ends up carrying three tooling charges that will never amortise at the volumes the line actually sells. Or the reverse: a brand forces five different shapes into one mould and discovers the shared part compromises every SKU it was meant to save.
This article explains how to spread mould cost across car fragrance SKUs without compromising the product. It covers the components of mould cost, single versus family moulds, interchangeable inserts, the amortisation arithmetic, and how to negotiate tooling with a factory so the tooling investment matches the sales reality.
Table of Contents
- Mould cost components
- Single versus family moulds
- Interchangeable inserts
- The amortisation arithmetic
- When to invest in tooling
- Negotiating with the factory
- Practical guide: amortising mould cost across SKUs
- Frequently asked questions
- Conclusion
Mould cost components
An injection mould's price is set by its steel grade, cavity count, and the complexity of the part it forms, not by the size of the finished product. A mould for a simple clip costs far less than one for a housing with fine texture, undercuts, and a moving slide. The cavity count matters most for amortisation: a one-cavity mould is cheap to cut but slow to run, while a multi-cavity mould costs more up front and produces several parts per cycle.
Beyond the steel, buyers pay for the engineering time, the trial shots, and any texture or polishing. These line items are where quotes differ, so ask for a breakdown rather than a single number. Two suppliers quoting the "same" mould can be quoting different steel, different cavity counts, or different trial provisions, and the difference only shows in the itemised version.
Single versus family moulds
A family mould produces multiple different parts in a single cycle, one cavity per part. The appeal is obvious — one tooling charge, several SKUs — but the economics come with a hidden constraint: all the parts in a family mould run together, so you produce them in fixed ratios even when their sales are not equal. If one SKU sells three times faster than the other, the slow seller piles up as excess inventory.
The fixed ratio is the reason family moulds often fail in practice. They work when the SKUs genuinely sell in proportion, such as a matched set of parts that always ship together. They backfire when the parts sell independently, because the mould forces you to over-produce the laggard or under-produce the leader. Match the mould structure to how the SKUs actually sell, not to how you hope they sell.
Interchangeable inserts
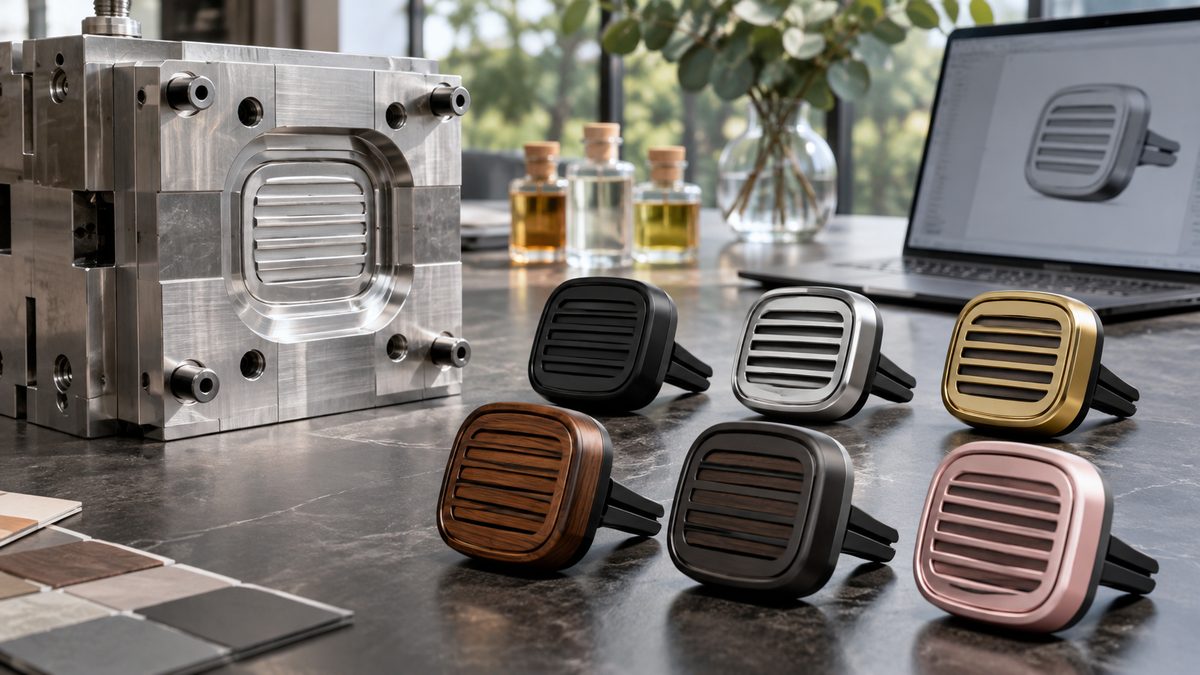
Interchangeable inserts are the middle path: a single mould frame with removable cavity inserts that swap out the differentiating feature, such as a logo or a surface pattern, while the shared geometry stays fixed. This amortises the frame across SKUs while keeping each variant's distinctive feature cheap to change. It is the standard approach when a range shares one housing but differs only in decoration or a small detail.
The insert approach has limits. The parts must share enough geometry that the frame works for all of them, and each new insert is itself a tooling cost, just a smaller one. Inserts amortise well when the variants are many and the changes small; they deliver less when every SKU needs a genuinely different shape.
| Approach | Tooling cost | Best for | Main risk |
|---|---|---|---|
| One mould per SKU | Highest | Genuinely different shapes | Tooling never amortises |
| Family mould | Moderate | Parts that ship in fixed ratio | Forced over-production |
| Shared frame + inserts | Lowest per variant | Shared housing, small changes | Variants must fit the frame |
The amortisation arithmetic
Amortisation is simple arithmetic dressed in uncertainty. Divide the tooling cost by the number of parts you will realistically mould from it over the product's life, and add the result to the per-unit moulding cost. That amortised figure is the true cost of the part, and it is what the selling price must cover before any margin appears.
| Volume assumption | Tooling cost | Amortised per unit |
|---|---|---|
| 5,000 units | High | High |
| 50,000 units | High | Low |
| 500,000 units | High | Negligible |
Reading the amortisation numbers
Using a range, not a point estimate
Because the lifetime volume is a guess, run the amortisation across a range rather than a single number. Calculate the amortised cost at a pessimistic, a realistic, and an optimistic volume, and check that the product still clears margin at the pessimistic end. If the tooling only pays off at the optimistic volume, you are betting the tooling on your best-case forecast, which is how tooling budgets quietly become losses.
When to invest in tooling
Invest in tooling when the amortised cost at a realistic volume is comfortably below the price premium the custom part supports, and when the part is genuinely a differentiator. A logo insert on a shared housing is usually a safe investment; a fully custom housing for a single low-volume SKU is usually not. The test is whether the custom part changes what a buyer is willing to pay, not whether it changes how the product looks.
Also weigh the alternative: a stock part with decoration often delivers most of the brand value at a fraction of the tooling. Before cutting steel, confirm there is no stock component that, with a printed or applied finish, gets the product to market for less. Tooling is the right answer when the stock option cannot deliver the differentiation, not when custom is merely preferred.
Negotiating with the factory
Tooling negotiation is about ownership and the trial terms, not just the price. Confirm in writing who owns the mould, where it is kept, and what happens if you change suppliers — a mould you paid for but cannot remove is not fully yours. Agree the trial-shot provision, the acceptance criteria, and who pays for revisions, because these terms decide the real cost far more than the headline figure.
Ask for the cycle time and piece rate alongside the tooling quote, because a cheap mould with a slow cycle costs more over the life of the part than a dearer mould that runs fast. For how these tooled parts fit the broader packaging decision, review our packaging options and our car fragrance pack planning guide. Our customisation process shows where tooling sits relative to formula and artwork approval.
Practical guide: amortising mould cost across SKUs
Step 1 — Map how the SKUs actually sell
Record the relative volumes of the range. The sales ratio, not the design, decides whether a family mould or separate moulds make sense.
Step 2 — Find the shared geometry
Identify what the SKUs genuinely share — a housing, a base, a clip — and what must differ. Shared geometry is where amortisation lives.
Step 3 — Choose the mould structure
Pick one mould per SKU, a family mould, or a shared frame with inserts, based on the sales ratio and the geometry.
Step 4 — Run the amortisation across a range
Calculate amortised cost at pessimistic, realistic, and optimistic volumes, and confirm margin at the pessimistic end.
Step 5 — Confirm ownership and trial terms
Put mould ownership, storage, trial shots, acceptance criteria, and revision costs in writing before you pay.
Step 6 — Get cycle time and piece rate
Request the cycle time and piece rate with the tooling quote, and compare total lifetime cost, not the mould price alone.
Frequently asked questions
What is injection moulding?
Injection moulding is a process that forces molten plastic into a shaped cavity to produce parts. The mould is the steel tool that forms the part, and its cost is a one-time investment amortised across the parts produced from it.
What is a family mould?
A family mould produces several different parts in one cycle, one cavity per part. It saves tooling cost but forces the parts to be produced in fixed ratios, which can over-produce slow sellers.
What is an interchangeable insert?
An interchangeable insert is a removable cavity piece within a shared mould frame that changes a specific feature, such as a logo, while the rest of the geometry stays fixed. It amortises the frame across many small variants.
How do I calculate amortised mould cost per unit?
Divide the tooling cost by the realistic lifetime volume and add the per-unit moulding cost. Run the calculation across a pessimistic, realistic, and optimistic volume rather than a single forecast.
When does a family mould make sense?
When the SKUs genuinely sell in proportion, so the fixed production ratio matches demand. If the parts sell independently and at different rates, a family mould forces over-production of the laggard.
Who owns the mould after I pay for it?
Ownership must be confirmed in writing before payment. Confirm that you own the mould, where it is stored, and that you can remove it if you change suppliers; a mould you cannot move is not fully yours.
Is a custom mould always better than a stock part?
No. A stock part with applied decoration often delivers most of the brand value at a fraction of the tooling cost. Invest in tooling only when the custom part changes what a buyer will pay, not just how the product looks.
Why should I ask for cycle time with a tooling quote?
Because a cheap mould with a slow cycle can cost more over the part's life than a dearer mould that runs fast. Compare total lifetime cost, not the mould price alone.
Conclusion
Mould cost is a forecasting problem wearing a manufacturing costume. The steel price is the visible number, but the real decision is whether the amortised cost clears margin at a volume you can actually sell — and whether the mould structure matches how the SKUs sell relative to each other.
Find the shared geometry first, choose the mould structure against the sales ratio, run the amortisation across a range, and lock ownership and trial terms in writing. Tooling done this way is an asset that pays for itself; tooling done on a best-case forecast is how a promising range quietly loses money.
Discuss your fragrance programme with our team:
WhatsApp: +86 17324762943
Email: adon@customperfumeoem.com
Website: customperfumeoem.com